Purpose-built for commercial distribution hubs along Nairobi’s Eastern Bypass, Mombasa Port transit freight terminals, and high-cube agro-cold facilities.
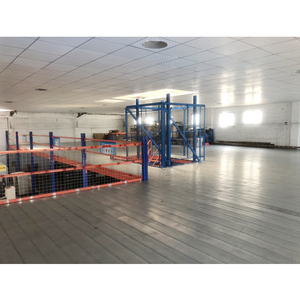
Multi-tier modular mezzanine platforms designed to double or triple usable square footage without structural building modifications in high-ceiling Nairobi warehouses.
View Specifications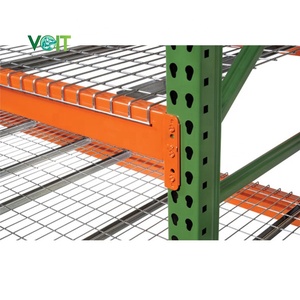
High-strength hot-dip galvanized wire decking panels that enhance sprinkler water penetration, fire safety compliance, and eliminate pallet point deflection.
View Specifications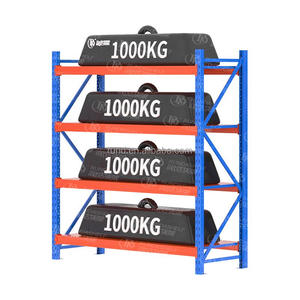
Flexible knockdown wire shelving systems suited for pharmaceutical stores, retail inventory buffers, and fast-moving small parts assembly lines across Kenya.
View Specifications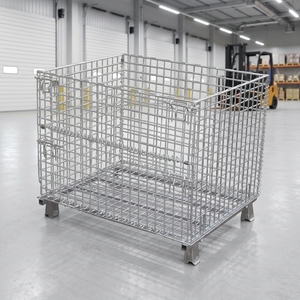
Collapsible wire stillages ideal for agricultural transport, automotive spare part sorting, and containerized multi-modal cargo transit between Mombasa and inland hubs.
View Specifications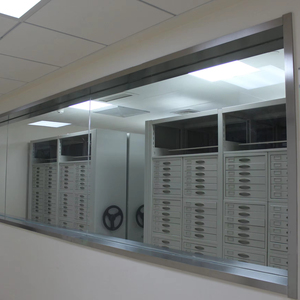
Micro-PLC controlled motorized compactors with infrared anti-pinch safety sensors, RFID integration, and optical safety bars for corporate, institutional, and medical archives.
View Specifications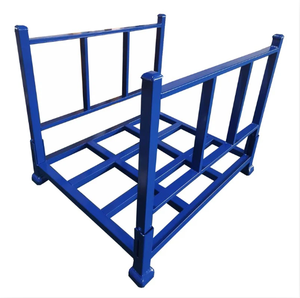
Interlocking post pallets for flexible, temporary seasonal storage surges in tea, coffee, and grain export warehouses without anchoring floor slabs.
View Specifications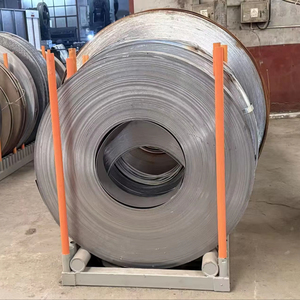
Heavy structural profile saddles engineered for cold-rolled steel, sheet metal, and wire coil master rolls, safeguarding round geometry against rolling hazards.
View Specifications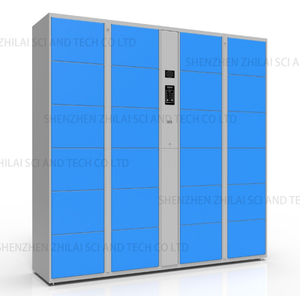
Automated barcode/PIN electronic locker banks fabricated from cold-rolled steel for logistics transfer checkpoints, staff locker rooms, and transport terminals.
View SpecificationsIndustrial Mobile Pallet Racking (also classified as Motorized Mobile Racking or Heavy-Duty Compactor Bases) represents the apex of structural density and mechanical engineering for modern Kenyan distribution facilities. Unlike conventional selective racking—which requires permanent, dedicated operating aisles for reach trucks and counterbalanced forklifts—an engineered mobile racking system places entire superstructure blocks onto electronically driven heavy-duty motorized steel carriages traversing flush or recessed floor guide rails.
In standard operation, opening a single working aisle (typically 3.0m to 3.5m wide) reveals 100% direct selectivity to pallet locations across dozens of contiguous bays. By condensing multiple aisles into a single dynamically variable aisle, facilities routinely achieve an 80% to 90% increase in storage capacity within the identical floor footprint, or eliminate 45% of total warehouse building construction costs on new greenfield developments.
Strategic material handling deployment tailored to the topography, logistics corridors, and industrial operating environments of Kenya.
Refrigerated and frozen food logistics hubs operating around Kilindini Harbour and Kipevu Special Economic Zones. Cold room mobile racking condenses cubic space, drastically slashing refrigeration power loads—a critical advantage given coastal electric tariffs and thermal cooling differentials.
Transit cargo bonded warehouses adjacent to the Embakasi Inland Container Depot (ICD) and Mombasa Road corridor. Accommodates surging cross-docking volume arriving from standard gauge rail (SGR) flatcars, ensuring rapid turnaround of FMCG goods and break-bulk imports.
Temperature-controlled packhouses and floricultural cold rooms in Naivasha and Eldoret. Mobile racking allows maximum cold-storage box density for export-grade cut flowers, fresh avocados, and herbs prior to rapid transport to Jomo Kenyatta International Airport (JKIA).
Pharmaceutical packaging, API stores, and cleanroom buffer hubs in Baba Dogo, Industrial Area, and Tatu City industrial parks. Facilitates high-density batch quarantine, strict FIFO inventory tracking, and full compliance with Kenyan Pharmacy and Poisons Board regulatory mandates.
Technical performance metrics for Kenya logistics engineers evaluating floor footprint allocation and capital ROI.
| Storage Racking System | Space Utilization | Pallet Selectivity | Aisle Requirement | Structural Floor Demand | Suitability for Kenya Cold Chains |
|---|---|---|---|---|---|
| Selective Pallet Racking | 40% - 50% | 100% (Individual Access) | High (One per rack row) | Standard C25/30 Concrete Slab | Low (High air-volume energy waste) |
| Drive-In Pallet Racking | 65% - 75% | Low (LIFO / Lane Only) | Low (Entry lane based) | Standard C25/30 Concrete Slab | Moderate (Prone to forklift collision damage) |
| Motorized Mobile Racking | 85% - 90% | 100% (Every Pallet Direct) | Single Floating Aisle | Laser-leveled embedded guide rails | Optimal (40% - 50% refrigeration reduction) |
| Multi-Tier Mezzanine Rack | 90%+ (Cubic) | 100% (Manual / Small SKU) | Vertical Stairs & Walkways | Point-load reinforced slab | Ideal for parts distribution & e-commerce picking |
Key structural catalysts driving the rapid transition to compact high-density automated racking throughout the East African community.
Prime industrial land prices along the Northlands Corridor, Tilisi, and Eastern Bypass have climbed exponentially. Investors can no longer afford expansive, single-level horizontal warehouses. High-bay industrial mobile racking maximizes vertical clear height up to 12 meters, allowing developers to compress total plot acquisition costs while doubling inventory density.
With industrial power tariffs in Kenya heavily influenced by fuel cost adjustments, refrigerated distribution centres are implementing rooftop photovoltaic (PV) solar systems coupled with high-efficiency variable-frequency drive (VFD) mobile chassis. Condensing cubic volume reduces chiller runtime hours, enabling cold stores to operate sustainably within off-grid solar and backup generator capacities.
Under the African Continental Free Trade Area (AfCFTA), Nairobi is solidifying its role as the East African logistical gateway serving Uganda, Rwanda, South Sudan, and eastern DR Congo. Regional bonded distribution hubs demand advanced warehouse management systems (WMS) tied to dynamic racking layouts to handle diverse multinational SKU profiles efficiently.
Decades of dedicated heavy fabrication, automated precision roll-forming, and strict structural conformance.
Over four decades of dedicated structural engineering and storage manufacturing. We operate direct automated production lines—not trading intermediaries—ensuring end-to-end metallurgical and dimension control.
Fabricated exclusively from certified high-tensile structural steel profiles. Beam sections, upright profiles, and mobile chassis plates are load-rated strictly according to international EN 15512 and FEM 10.2.07 standards.
Continuous CNC roll-forming lines with multi-station punching ensure uniform pitch accuracy (±0.5mm), flawless bolt alignment, and rapid modular assembly on site without on-field cutting or welding.
Automated pre-treatment phosphating and electrostatic epoxy-polyester powder coating cured at 200°C. For high-humidity coastal Mombasa facilities, we deliver full hot-dip galvanization ensuring 25+ years rust resistance.
Engineered modular knockdown packaging maximizes shipping container volume (40ft High Cube), slashing ocean freight costs to Kilindini Harbour, Mombasa, with zero transit deflection or scratching.
Proven track record supplying complex racking and compactor installations across the Middle East, Canada, Bahrain, Sri Lanka, and East Africa, backed by comprehensive CAD/3D layouts and on-site assembly guidance.
Essential technical, seismic, import clearance, and foundation criteria for engineering teams in Kenya.
