
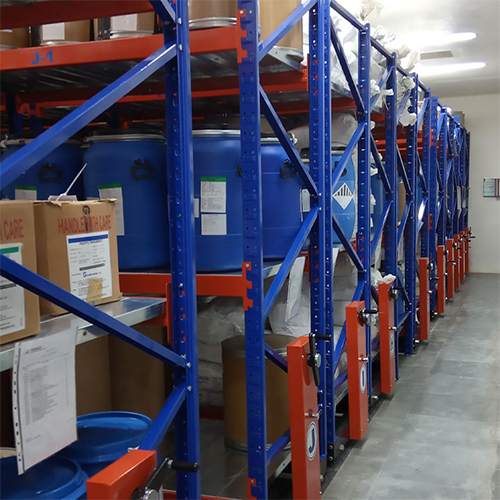
Engineering Excellence & Space Optimization Principle
In standard selective pallet racking installations, up to 60% of total warehouse surface area is dedicated strictly to access aisles for material handling equipment. Divakaran's Industrial Mobile Racking System reclaims valuable square meters by positioning racking bays onto motorized mobile bases that glide across precision-aligned floor tracks.
By moving rows together, multiple aisles are condensed into a single dynamic access corridor that opens automatically or mechanically whenever an operator requires access. This methodology increases pallet position density by up to 85%-90% compared to traditional static configurations, making it the premier choice for land-constrained facilities, refrigerated distribution networks, and temperature-controlled cold vaults.
85% Floor Utilization
Reclaims obsolete corridor space into active storage volume, substantially lowering cost-per-pallet position.
Cold Chain Energy Saver
Reduces air volume requirements in refrigerated and sub-zero storage by up to 40%, cutting ongoing utility bills.
Intelligent Safety Arrays
Integrated optical safety beams and base-mounted emergency stops immediately halt carriage motion if an obstruction is detected.
Custom Heavy Bay Loadings
Engineered upright columns and boxed load beams sustain high pallet tonnage without mechanical distortion.
Modular Growth Scalability
Modular rail base design allows easy track extensions and superstructure bay additions as product throughput increases.
Export-Grade Precision
Manufactured on calibrated roll-forming equipment in Umbergaon, Gujarat, ensuring smooth assembly at international job sites.
Technical Specifications & Design Criteria
| System Parameter | Standard Specification | Heavy-Duty / Cold Store Specification |
|---|---|---|
| Load Capacity Per Bay | Up to 6,000 kg (Uniformly Distributed Load) | Custom engineered up to 15,000+ kg per mobile base |
| Standard Heights | 3,000 mm to 4,500 mm (up to 15 ft) | Custom heights designed according to warehouse clear eaves |
| Drive Motor Options | 0.37 kW to 0.75 kW synchronous geared motors | IP55/IP65 low-temperature rated inverter-driven gearboxes |
| Floor Rail System | Surface mounted with chamfered ramps | Precision embedded flush-to-slab rails with anti-wear alloy |
| Carriage Base Steel | Heavy-gauge folded high-tensile structural channel | Hot-rolled structural channel with rust-inhibiting zinc primers |
| Aisle Opening Speed | Approx. 3.5 to 5.0 meters per minute | Variable speed frequency control for smooth starting/stopping |
| Operating Temperature | -5°C to +45°C ambient warehouse conditions | -30°C to +10°C continuous deep freezer operation |