Heavy-Duty High-Density Storage

Mobile Compactor System

Precision-engineered rail-guided mobile shelving systems designed to eliminate idle aisle space, dramatically maximizing cubic capacity in warehouse archives, tool rooms, healthcare, and financial institutions.

Space Optimization Technology

Engineered High-Density Compactor Solutions

Manufactured under stringent ISO-aligned quality controls in Umbergaon, Gujarat, our mobile compactor systems deliver seamless mechanical drive operation, integrated safety locking mechanisms, and robust load capacities built for demanding commercial environments.

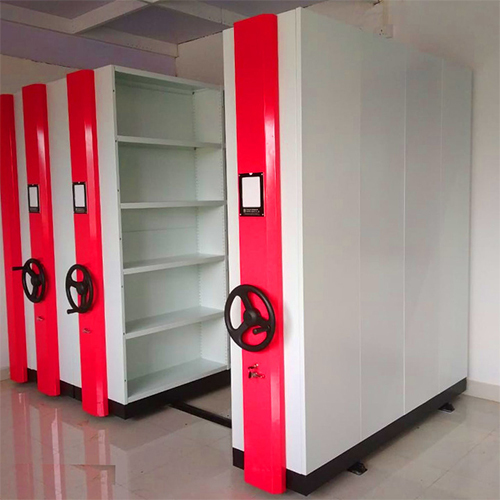
Ease of Access Mobile Compactor System installed in commercial record room

Ease of Access Mobile Compactor System

Designed for fast-turnaround retrieval, offices, medical record archives, and light-to-medium parts logistics. Featuring smooth low-friction hand wheels, anti-tip floor guides, and centralized key locks for secure corporate archiving.

Application High-Density Material & Document Storage
Construction Prime Cold-Rolled Structural Steel / SS Finish
Height Profiles Up to 10 Feet (Customized to Ceiling Clearances)
Drive Mechanism Ergonomic Mechanical Reduction Gearbox
Shelf Adjustability 25mm Increment Flexible Pitch
Surface Finish 7-Tank Pretreatment Powder Coating (RAL Shades)
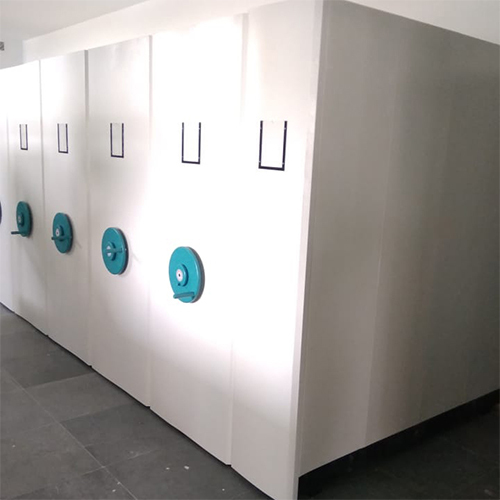
Industrial Mobile Compactor System with heavy duty steel chassis and rails

Industrial Mobile Compactor System

Reinforced high-load capacity mobile racking tailored for manufacturing plants, automotive spare distribution, raw materials, and tool rooms. Engineered with solid steel track bases to withstand high tonnages per carriage.

Application Industrial Spares, MRO Goods & Heavy Tools
Construction Heavy-Section Structural Steel Base Carriages
Rail Foundation Surface Ramped or Concrete Embedded Low-Profile Tracks
Safety Systems Mechanical Gangway Locks, Aisle Lockers & Rubber Bumpers
Carriage Capacity Up to 1,200 kg per Storage Bay
Export Compliance CKD Knock-Down Palletized Container Packaging

80% Space Recovery

Consolidates multiple static aisles into a single movable gangway, reducing required footprint by up to 80% or doubling inventory in the same room.

Confidential & Secure

Equipped with central key locking systems and individual carriage locks to protect sensitive files, pharmaceutical items, and high-value equipment from unauthorized access.

Smooth Gear Transmission

Precision sprocket-and-chain drive systems with high-torque gear reduction permit effortless gliding of thousands of kilograms with light finger effort.

Dust & Pest Resistance

Neoprene sealing strips along bay intersections form a closed compartment when compacted, defending stored documents and assets against light, dust, and pests.

Engineering Rigor

Robust Mechanical Design & Architectural Adaptability

At Divakaran, our mobile storage solutions are designed for longevity, durability, and smooth mechanical responsiveness. We address diverse architectural floor limits with custom track designs and calibrated wheel assemblies.

  • Heavy-Gauge Sub-Bases: Welded, distortion-free chassis constructed from cold-formed channel steel for lifetime rail alignment.
  • Sealed Ball Bearing Wheels: High-tensile forged steel wheels running on dual sealed bearings for silent traversing under capacity loads.
  • Modular Track Profiles: Choice of sunken tracks flushed with screed floor, or surface-mounted rails with integrated anti-trip aluminum ramps.
  • Export-Ready Knockdown Packaging: Bolt-together modular bays designed for compact container packing, reducing ocean freight costs.
Technical Attribute Industrial Grade Commercial / Archive Grade
Standard Bay Heights 1,800 mm to 3,000 mm 1,800 mm to 2,400 mm
Shelf Widths / Bay 900 mm, 1,000 mm, 1,200 mm 900 mm, 1,000 mm
Shelf Depths 300 mm to 600 mm (Single/Double) 300 mm to 450 mm
Uniform Distributed Load (UDL) 150 kg – 350 kg per shelf 60 kg – 120 kg per shelf
Braking & Lock Mechanism Foot brake + Central Gangway Lock Rotary Lock + Push Safety Plunger
Finish Electrostatically applied epoxy Antimicrobial powder coat (optional)

Require an Optimized Layout for Your Facility?

Send our project engineering team your room architectural drawings and SKU parameters. We will produce a complete 2D/3D storage layout with bay calculations within 48 hours.

Get a Quote
Technical FAQ

Frequently Asked Engineering Inquiries

Key information regarding structural floor load requirements, track options, and export handling for international warehouse and logistics managers.

What floor preparations are required for installing mobile compactors?
Mobile compactor systems consolidate inventory weight over smaller areas, requiring a level, structurally sound slab. If civil alterations are not permitted (e.g. rented premises), we provide surface-mounted rail systems with false flooring and ramps that preserve existing floor tiles. For new projects, grouted floor-recessed channels offer flush movement for trolley access.
How does a mobile compactor optimize storage capacity compared to static racks?
Static shelving requires a dedicated 800mm to 1,000mm gangway between every two racks. A mobile compactor system moves the entire bank of shelves together, requiring only one floating aisle that opens wherever needed. This eliminates redundant aisle waste and delivers 50% to 80% higher density.
What security and operator safety systems are engineered into the carriages?
Each mobile carriage is fitted with a rotary hand wheel lock so operators can lock the open aisle while accessing materials. Rubber bumpers cushion carriage impact, anti-tip floor interlocks prevent tipping during floor loading variations, and master key cylinder locks secure all units in the compressed position.
Can Divakaran manufacture custom dimensions and export abroad?
Yes. As an established direct manufacturer in Gujarat since 1977, we fabricate customized configurations built around specific ceiling heights, column locations, and floor plans. All components are packed in CKD knockdown form with international export strapping and waterproof wrapping.