OEM/ODM Intralogistics Manufacturing Excellence Since 1977
Top Trusted Automated Storage System Factory & Supplier
Heavy-Duty Automated Pallet Racks, Intelligent Electric Mobile Storage, and Engineered Structural Mezzanines Fabricated to Rigorous FEM, RMI & ISO Standards.
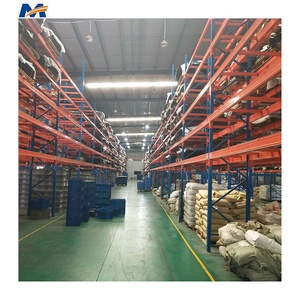
Fabricated from prime Q235B and Q345B structural steel at our Umbergaon manufacturing plant, each modular configuration delivers certified load capacity, seamless WCS/WMS handshake compatibility, and maximum cubic space utilization.
Regular export dispatches to Bahrain, UAE, Saudi Arabia, Oman, Sri Lanka, Canada, and Europe.
0.0%
Structural Failures
Rigorous finite element analysis (FEA) and destructive batch testing across every production cycle.
Procurement Engineering Whitepaper
Engineering Principles of Automated & High-Density Storage
Modern warehousing demands more than static steel shelves. Specifying automated storage systems requires an exhaustive evaluation of load dynamics, floor slab deflection tolerances, SKU throughput frequencies, and material handling fleet compatibility.
Structural Steel Metallurgy & Cold Roll-Forming
Reliability starts at the metallurgical level. At our Umbergaon, Gujarat plant, we process certified prime coils of Q235B and Q345B structural steel (equivalent to ASTM A36 and S355JR). Roll-formed uprights feature continuous multi-bend profiles engineered to resist lateral torsional buckling under maximum dead-plus-live seismic load envelopes.
Yield Strength: Guaranteed minimum yield point of 345 MPa for critical upright columns.
Hole Pitch Precision: 50mm and 75mm CNC punched slots with ±0.2mm tolerance for beam locks.
Pre-treatment: 7-tank chemical degreasing, zinc-phosphating, and hot shot-blasting to SA 2.5 cleanliness.
Electric Mobile Automation & PLC Integration
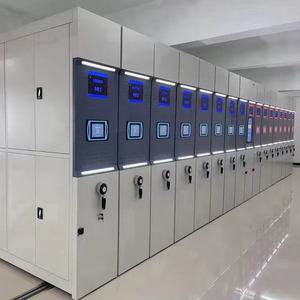
By eliminating dedicated forklift access aisles, Intelligent Electric Mobile Racking (EMR) converts up to 85% of total warehouse floor footprint into usable storage. Our motorized bases operate on precision-leveled floor embedded guide rails driven by modular asynchronous gearmotors synchronized via industrial fieldbus networks.
WMS Direct Handshake: Automated aisle opening orchestrated via picking list algorithms.
Cold Chain Optimized: Drive assemblies rated for sub-zero operation down to -30°C in food/pharma.
FEM & RMI Design Safety Compliance
Storage structures must withstand non-uniform vertical loading, dynamic seismic acceleration, and accidental forklift mast impacts. Our engineering group executes comprehensive 3D stiffness modeling strictly adhering to FEM 10.2.02, EN 15512, and RMI (Rack Manufacturers Institute) specifications.
Safety Deflection Limits: Main load-bearing beam deflection strictly restricted to ≤ L/200.
Safety Factor: Certified minimum structural factor of safety ≥ 1.65 under design loads.
Seismic Baseplates: Heavy-gauge anchor baseplates designed for dynamic shear transmission.
Engineering Specifications
Industrial Storage System Selection Matrix
Evaluate key performance parameters to select the optimal intralogistics platform for your warehouse facility:
Global supply chain disruptions and surging real estate expenditures have permanently altered capital expenditure priorities for warehousing infrastructure. Forward-thinking procurement managers are executing long-term strategies focused on flexibility, modularity, and operational resilience:
Shift Towards Knock-Down Container Optimization: Surging ocean freight rates prioritize bolted prefab structures that pack tightly into standard 40ft High Cube containers, minimizing landing costs for international export projects.
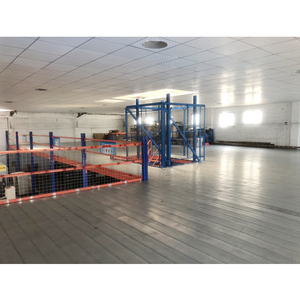
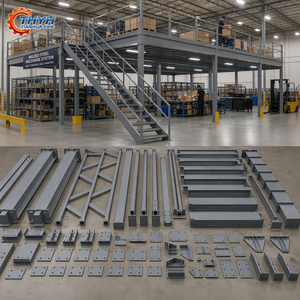
Near-Zero Footprint Civil Expansion: Instead of leasing external warehouses, enterprises are leveraging multi-tier rack-supported mezzanines to vertically densify operations within existing building envelopes.
Cold-Chain & Cleanroom Specification Surge: Expanding biologic pharmaceuticals and frozen food processing demand food-grade stainless steels (SS 304/316) and high-cure TGIC powder finishes impervious to chemical washdowns.
Total Cost of Ownership (TCO) Mandates: Procurement audits increasingly weigh salvage value, modular reconfiguration speed, and structural steel recycling credit against upfront purchase cost.
Intralogistics Technological Evolution
The convergence of industrial automation, smart robotics, and real-time telemetry is transforming passive storage frames into active nodes of warehouse intelligence. As a premier original equipment manufacturer, our R&D pipeline incorporates emerging operational technologies:
Structural Health Monitoring (SHM) Telemetry: Integration of fiber-optic strain gauges and triaxial accelerometers on critical uprights to record minor forklift impacts and monitor structural fatigue in real time.
AMR & AGV Surface Alignment: Engineering zero-threshold decking transitions and laser-calibrated ground track tolerances to enable frictionless collaboration between Autonomous Mobile Robots and mobile bases.
Digital Twin Engineering Models: Delivering comprehensive 3D BIM (Building Information Modeling) and structural CAD geometries that plug directly into enterprise ERP and spatial management engines.
Green Steel & Eco-Coating Chemistry: Transitioning production lines to lower-carbon electric arc furnace (EAF) steel coils coupled with heavy-metal-free, zero-VOC electrostatic powder curing technologies.
Engineered in Umbergaon, Gujarat – Trusted by Global Leaders
Divakaran Storage and Handling Systems Pvt. Ltd. has continually manufactured turnkey storage platforms for prestigious EPC contracts, government utilities, and multi-national corporations. Our products safeguard hundreds of thousands of metric tons of inventory every day.
Clear, definitive technical guidance addressing the most common design, logistic, and structural specifications encountered by overseas engineering teams and supply chain procurement officers.
What engineering input parameters are required to generate an optimized warehouse racking layout?
To provide a certified technical proposal, our engineering office requires: (1) Architectural floor plan DWG indicating building column grid, clear ceiling heights under roof trusses, emergency exits, and overhead sprinkler headers; (2) Detailed pallet load profile including length, width, overall height including cargo overhang, and maximum pallet gross weight; (3) Existing or planned Material Handling Equipment (MHE) specification sheet indicating forklift type, turning radius, mast collapsed height, and aisle clearance requirement; (4) Concrete floor slab data including compressive strength rating (e.g., C25/30 or C30/37), rebar placement, and slab thickness; and (5) Local seismic zone spectral acceleration coefficients (Ss and S1).
How does your Umbergaon manufacturing plant verify structural load compliance and weld integrity?
Quality assurance encompasses raw material chemical and mechanical tensile testing per IS 2062 / GB Q235B & Q345B standards. Upright frames and connector clips undergo destructive push-pull and stub-column testing to empirically validate rotational spring stiffness parameters. Robotic welding stations undergo periodic dye-penetrant inspection (DPI) and magnetic particle testing (MPT) for joint integrity. Finished electrostatic powder coatings undergo cross-hatch adhesion testing (ASTM D3359) and 500-hour continuous neutral salt spray testing (ASTM B117) to guarantee corrosion protection.
How are heavy storage systems packaged to maximize ocean freight efficiency and prevent transit corrosion?
All heavy-duty pallet racking and mezzanine components are produced in knock-down (KD) configurations. Upright frames are either shipped disassembled or flat-stacked with protective corrugated spacers. Beams are bundled in matched length sets with heavy-duty polyester strapping and reinforced timber dunnage to avoid steel-on-steel friction. Hardware, anchor studs, baseplates, and leveling shims are packed in labeled seaworthy wooden cases. All ocean shipments incorporate heavy VCI (Vapor Corrosion Inhibitor) plastic wrapping and desiccant packs to endure maritime humidity across multi-week shipping routes to Bahrain, Saudi Arabia, Europe, or Canada.
Can your structural steel mezzanine platforms be relocated or expanded if operational needs change?
Yes. Our structural mezzanine floors utilize a 100% mechanical bolt-connected design using high-tensile Grade 8.8 or 10.9 structural fastener sets. Zero field welding is required during assembly. This modular architecture allows systems to be seamlessly unbolted, relocated, reconfigured in shape, or extended with additional column bays as inventory volumes expand, safeguarding capital investment over multi-decade facility leases.
What are the civil floor slab requirements for installing Intelligent Electric Mobile Racks?
Electric Mobile Racking concentrates dynamic wheel loads along specific floor tracks. Depending on overall bay height and load weight (which can reach 24 tons per mobile carriage), the warehouse concrete floor typically requires a minimum thickness of 180mm to 250mm with a compressive rating ≥ 30 N/mm² (C30/37). Guide rails can be cast directly into initial floor screeds during new construction or retrofitted into existing warehouses via diamond precision saw-cutting, non-shrink structural epoxy grouting, and optical leveling to within ±1.0mm per 10 meters of rail length.
How does your factory accommodate fire suppression sprinkler systems within high-density racks?
Our engineering layouts strictly comply with NFPA 13 (Standard for the Installation of Sprinkler Systems) and FM Global data sheets. We calculate systematic vertical and horizontal flue spaces (typically 150mm clear minimum) between adjacent pallet backs and side frames. Upright column geometry is designed to allow integrated in-rack sprinkler pipe bracket clamps without compromising structural beam-locking slots or reducing usable pallet lift clearance.
What is the standard production lead time for international custom export orders?
Upon approval of final engineering layout drawings and structural calculations, standard manufacturing lead times range between 3 to 5 weeks for orders of 2 to 10 standard 40ft High Cube containers. Highly specialized automated projects involving motorized electrical drive carriages or customized stainless steel cleanroom systems typically require 6 to 8 weeks to permit factory acceptance testing (FAT) of PLC control cabinets and sensor telemetry before packing.
Do you supply on-site installation supervision and international commissioning engineers?
Yes. For international export clients, we provide two execution models: (1) Turnkey installation management, deploying our certified mechanical and electrical rigging supervisors to manage local work crews; or (2) Comprehensive remote engineering support, providing step-by-step 3D exploded assembly diagrams, detailed anchor torque tables, video documentation, and real-time remote engineer oversight.
How do Cantilever Racks handle non-uniform or variable-length industrial inventory?
Cantilever systems eliminate front upright obstruction, allowing continuous horizontal linear storage. Our cantilever arms attach to heavy I-beam or cold-formed columns via heavy-duty retaining pins or high-strength bolts, allowing arm height adjustments on 100mm increments. Removable steel end-stops prevent tubular items (such as copper pipes and steel conduits) from rolling off, while optional wire mesh or solid steel shelf decking can be installed across arm tiers to accommodate varying package lengths simultaneously.
What warranty terms and structural maintenance coverage are supplied with your factory systems?
All Divakaran structural steel components (uprights, beams, bracing, structural mezzanine frameworks) carry a comprehensive 5-year structural integrity warranty against manufacturing defects and weld degradation under rated loading conditions. Motorized electrical drive assemblies, PLC electronics, and sensors for intelligent mobile racking carry a 1-year replacement warranty, with extended maintenance contracts and rapid-dispatch replacement part inventories available for global clients.