Discover enterprise-grade motorized mobile compactors, heavy-duty industrial mobile racks, and specialized material storage custom-fabricated for North American industrial facilities.
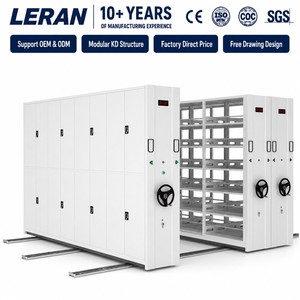
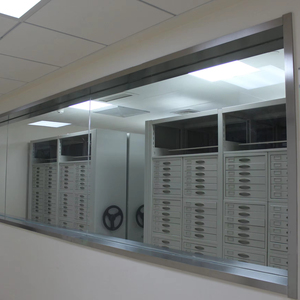
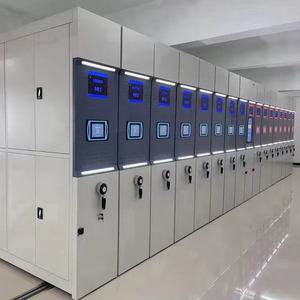
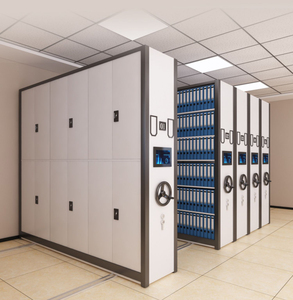
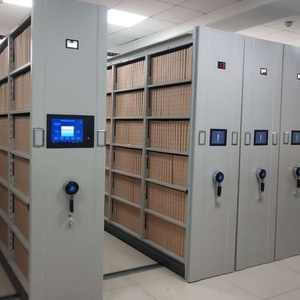
Across major logistics infrastructure corridors in the United States—ranging from the Inland Empire in Southern California and the Dallas-Fort Worth metroplex to Chicago’s industrial belt and the New Jersey Turnpike distribution nodes—industrial real estate costs continue to soar. Prime warehouse space premiums have compelled supply chain executives and facility managers to abandon static, space-inefficient storage layouts. Standard selective pallet racking layouts consume up to 60% of total square footage in dedicated forklift operator aisles. Electric Mobile Racks (EMR), also referred to as motorized mobile pallet racking or automated high-density mobile shelving, solve this structural inefficiency by placing heavy-duty racking bays onto heavy-steel guided mobile carriages.
These motor-driven mobile bases travel along precision-milled structural steel rails embedded flush into or anchored onto concrete floor slabs. By opening a singular operational aisle dynamically via PLC microprocessors, touch-screen interfaces, radio-frequency remote units, or integrated voice commands, facilities can eliminate fixed aisles completely. This delivers an immediate 80% to 100% expansion in total usable pallet positions within the identical building footprint, or conversely, reduces required construction square footage by half for newly planned logistics parks.
Deploying heavy-duty motorized racking in North America demands strict engineering compliance with the Rack Manufacturers Institute (RMI) specification MH16.1 (Specification for the Design, Testing and Utilization of Industrial Steel Storage Racks) and local International Building Code (IBC) provisions. Because electric mobile racks carry massive moving payloads—often exceeding 24,000 lbs (11,000 kg) per bay and up to 48,000 lbs per movable double-rack carriage—structural dynamics under kinetic movement and seismic accelerations require specialized structural analysis.
Our manufacturing engineering team utilizes structural steel grade Q235B/Q355B with calibrated gauge thicknesses, heavy-duty column uprights, and dynamic seismic locking mechanisms. In high-risk USGS seismic zones (such as California, Western Washington, and the New Madrid Seismic Zone), our mobile carriages incorporate mechanical floor-anchored anti-tip systems, dual-drive synchronised motor shafts, and automatic dynamic braking to prevent load shift during seismic events.
Built for 24/7 continuous industrial operation, severe cold-chain environments, and automated smart facility integration.
Fabricated using structural cold-rolled steel with custom frame profiles. Upright columns and heavy-duty roll-formed beams are powder-coated or galvanized for long-term corrosion resistance and heavy impact endurance.
Compliant with North American industrial safety guidelines. Features optical photoelectric safety curtains across aisle openings, emergency push-stop buttons, bumper touch-sensors, and automatic obstacle deceleration.
Siemens or Allen-Bradley PLC control modules support seamless integration via EtherNet/IP or Modbus TCP/IP into automated Warehouse Management Systems (WMS), enabling pre-opening of aisles via forklift-mounted RFID terminals.
Specially engineered low-temperature motors, cold-climate synthetic lubricants, IP65-rated control panels, and anti-condensation heating cables designed to optimize high-density refrigerated logistics and frozen food hubs.
Offers flat-rail and surface-mounted rail configurations. Options include direct embedding during fresh concrete slab pours or diamond-cut trench retrofitting into existing industrial floors with non-shrink epoxy grouting.
Equipped with intelligent voice recognition modules and multi-channel handheld wireless controllers, allowing hands-free command execution for pick-and-pack crews, enhancing overall warehouse order velocity.
Evaluate how Electric Mobile Racking compares against traditional and semi-automated warehouse storage formats used across US facilities.
| Storage Racking Architecture | Footprint Efficiency | Direct SKU Selectivity | Cold Storage Energy ROI | Seismic Safety Suitability |
|---|---|---|---|---|
| Electric Mobile Racking (EMR) | Very High (85%–90%) | 100% Direct Access | Maximum (Saves 40% Cooling Costs) | Excellent (With Dynamic Locking) |
| Standard Selective Racking | Low (40%–45%) | 100% Direct Access | Poor (High Air Cube Waste) | Standard Anchoring |
| Drive-In / Drive-Thru Racking | High (65%–75%) | Very Low (LIFO Only) | Moderate | Requires Heavy Top Bracing |
| Double-Deep Selective Racks | Medium (55%–60%) | 50% Direct Access | Moderate | Requires Specialized Forklifts |
| Pallet Shuttle (Automated) | Very High (80%–88%) | Low (Deep Lane LIFO/FIFO) | High | Requires High Rigidity Structural Steel |
Our motorized mobile storage solutions are tailored to meet strict regulatory and operational workflows across key US industry sectors:
In cold storage facilities where utility costs for cooling expansive building volumes represent the primary operating expense, Electric Mobile Pallet Racking provides massive financial returns. By consolidating frozen inventory into a compact block, operators reduce refrigerated vault volume requirements by up to 50%. This direct reduction in thermal dissipation lowers compressor power usage dramatically while preserving 100% selective access for strict FDA track-and-trace compliance.
US pharmaceutical warehouses operating under strict cGMP guidelines demand climate-controlled, secure, and fully auditable storage. Intelligent electric mobile shelving units feature electronic PIN access, audit-log record tracking, and seamless software integration with automated picking systems. Cleanroom-compatible powder finishes ensure dust-free operation for sensitive healthcare products.
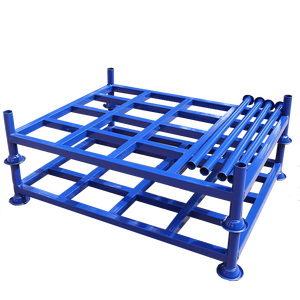
For automotive assembly plants and Tier-1 suppliers across the American Midwest and Sunbelt regions, dense component storage is vital. Heavy-duty mobile racks handle industrial steel totes, dies, engine blocks, and customized fabric roll containers (such as CASE CARTER OEM stackable racks), maintaining high floor load capacities up to 24,000 lbs per bay without base deflection.
High-density motorized dense cabinets and voice-controlled 5-tier mobile shelving units provide law firms, financial institutions, government agencies, and university libraries with ultra-compact document archival solutions. Integrated micro-sensors protect paper records from compression or light damage while maximizing room storage volume.
Over 45 Years of Structural Metal Storage Engineering (Established 1977)
Founded in 1977, our manufacturing heritage spans more than four decades of dedicated innovation in industrial storage systems, structural pallet racking, motorized mobile compactors, and heavy-duty material handling equipment. Operating from our advanced manufacturing industrial complex in Umbergaon, Gujarat, our facilities combine automated CNC cold-roll forming lines, robotic welding cells, and eco-friendly automated powder coating plants.
Every structural column, beam, and mobile carriage base is manufactured using premium structural steel grades, rigorously tested for tensile strength, load-deflection ratios, and impact resistance.
Our engineered racking solutions are trusted internationally, with major installations deployed across North America (United States, Canada), the Middle East, Bahrain, Sri Lanka, and worldwide logistics hubs.
From initial CAD space planning and seismic calculation reports to site supervision, containerized knock-down delivery, and long-term preventive maintenance, our engineering team ensures seamless execution.
Everything you need to know about specs, seismic codes, floor requirements, and ordering electric mobile racks for US operations.
Consult with our senior structural engineers to receive customized CAD layouts, structural engineering calculations, and competitive direct-factory quotations tailored for your US facility.
Inquire Now