High-performance pallet racking, heavy-duty mezzanine structures, and automated high-density systems engineered for global compliance and seamless logistics export to New Zealand ports.
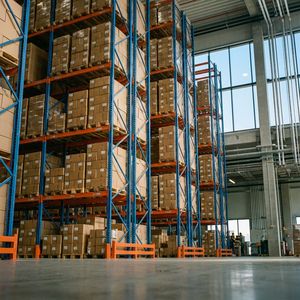
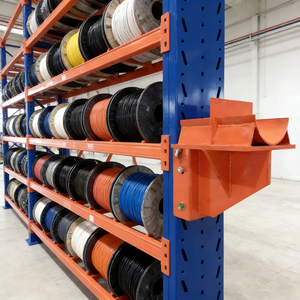
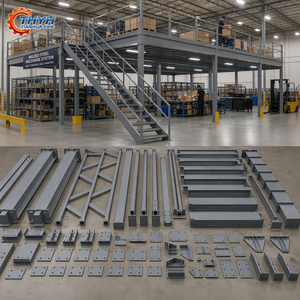
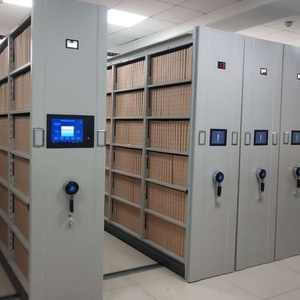
Industrial logistics operations across New Zealand face severe spatial constraints, driven by soaring commercial real estate values in urban centers like South Auckland (Wiri, Mount Wellington, Highbrook) and Christchurch (Hornby, Islington). To maximize volumetric floor area, logistics directors and industrial structural engineers are increasingly shifting from conventional selective pallet racking to Drive-In Pallet Racking Systems. Manufactured engineered drive-in systems operate on the Last-In, First-Out (LIFO) inventory accumulation principle, eliminating working aisles to consolidate up to 85% of standard warehouse void space.
Unlike standard frame configurations where forklifts operate within designated exterior aisles, drive-in pallet racking allows counterbalanced or reach trucks to drive directly into the structural rack lanes. Pallets rest on continuous cantilevered support rails mounted on heavy-duty cold-formed upright frames. This dense racking philosophy is ideal for homogeneous bulk goods, cold storage facilities, primary produce packhouses, and high-volume dairy export staging environments prevalent throughout New Zealand's agricultural export supply chain.
Because forklifts enter the internal matrix of a drive-in system, traditional cross-beam horizontal bracing within the storage lanes is absent. Consequently, structural integrity relies entirely on rigid top tie-beams, back bracing frames (in Drive-Through configurations or rear walls), double-anchored baseplates, and high-torsion upright profiles. Our systems utilize ultra-high-yield strength structural steel (Q235B and Q355B structural grades), precision-engineered to withstand continuous horizontal dynamic impact loads and vertical static pallet loads up to 1,500 kg per position.
| Racking System Type | Volumetric Efficiency | Access Philosophy | Aisle Space Required | NZ Seismic Rating Suitability | Best NZ Industry Application |
|---|---|---|---|---|---|
| Drive-In Pallet Racking | 75% – 85% Maximum Density | LIFO (Last-In, First-Out) | Minimal (Entry Bay Only) | High (Custom Top & Rear Bracing) | Cold Stores, Dairy Export, Kiwifruit |
| Selective Pallet Racking | 35% – 45% Standard Density | FIFO (100% Direct Access) | High (3.0m - 3.8m Aisle Width) | Standard AS/NZS 4084:2012 | FMCG, General 3PL, Retail Distribution |
| Double-Deep Racking | 55% – 65% Medium Density | FILO (50% Direct Access) | Medium (Pantograph Reach Truck) | Moderate to High Structural Rigidness | Pharmaceuticals, Industrial Packaging |
| Pallet Shuttle (Radio Shuttle) | 80% – 90% Ultra Density | LIFO or FIFO Automated | Minimal (Front Access Only) | Very High (Lower Dynamic Impact) | High-Volume Deep Freeze & Beverage Hubs |
New Zealand lies directly on the volatile Pacific Ring of Fire. Following historical seismic events such as the Canterbury and Kaikoura earthquakes, WorkSafe NZ and local municipal councils enforce stringent structural design standards. All storage racking systems installed across the North and South Islands must satisfy AS/NZS 4084:2012 (Steel Storage Racking), NZS 3404 (Steel Structures Standard), and AS/NZS 1170 (Structural Design Actions).
Engineered drive-in systems exported by factory manufacturers to New Zealand incorporate specialized seismic mitigation features designed to prevent structural sway, frame buckling, and unseating of loaded pallets during severe horizontal accelerations (PGA values):
Heavy-duty, oversized steel baseplates fitted with dual expansion structural anchors engineered to withstand high shear forces and vertical uplift moments caused by earthquake acceleration vectors.
Formed cantilever support rails feature flared entrance guides and mechanical anti-dislodgement stops. This ensures smooth forklift entry while locking pallets securely in position during ground motion.
Rigid portal frame ties spanning across the top of the drive-in bays distribute lateral wind and earthquake loads throughout the structural lattice, mitigating dynamic torsional movement.
Custom-engineered Drive-In Pallet Racking systems serve critical operational hubs across New Zealand. Factory direct manufacturing allows tailoring bay dimensions, depth profiles, structural gauges, and surface coatings to the micro-climate and material handling demands of distinct NZ regions:
Context: Controlled-atmosphere deep-freeze warehouses operating at -25°C require maximum pallet density to minimize electrical refrigeration costs per cubic meter.
Engineering Solution: Drive-In racking configured 6 to 10 pallets deep with heavy-duty hot-dip galvanized finishes or specialized low-temperature powder coatings. Protects steel from thermal shock condensation while storing bulk frozen butter, cheese blocks, and milk powder export pallets bound for Port of Tauranga and Lyttelton Port.
Context: Seasonal harvest surges in Te Puke, Tauranga, and Hastings generate intense short-term storage demands for thousands of uniform produce trays.
Engineering Solution: High-volume drive-in lanes matching standard New Zealand wooden pallets (1200mm x 1000mm CHEP/Loscam). Allows rapid batch load staging during peak harvesting months, enabling FIFO or LIFO rotation prior to refrigerated container shipping.
Context: Logistics distribution centers in Wiri, Highbrook, and Auckland Airport precinct face high cost-per-square-meter warehouse leases.
Engineering Solution: Drive-In systems fitted with heavy-duty column protection guards and floor-mounted forklift guide rails. Facilitates fast driver entry, protecting rack uprights from accidental collision while doubling warehouse pallet capacity without expanding physical floor space.
As New Zealand modernizes its logistics infrastructure, several key macroeconomic trends dictate warehouse storage design and international procurement strategies:
Established in 1977, Divakaran Storage and Handling Systems Pvt. Ltd. brings over 45 years of structural steel manufacturing authority. Operating an advanced automated manufacturing facility at Umbergaon, Gujarat, India, our engineering firm specializes in designing, fabricating, and exporting high-capacity industrial racking systems to demanding international markets including New Zealand, Australia, Canada, Bahrain, Sri Lanka, and the Middle East.
Fabricated from certified Q235B and high-tensile Q355B structural steel grades. All components undergo rigid structural analysis, shot-blasting surface pretreatment, and thermosetting epoxy-polyester powder coating for maximum corrosion resistance.
Our in-house design team produces full 3D CAD layouts, structural load calculations, and seismic frame bracing configurations tailored to specific New Zealand earthquake zones (Zone 1 to Zone 4).
Knock-down modular components are bundled with steel strapping, protective edge cornering, and sea-worthy moisture barriers. Direct ocean freight container shipping to Ports of Auckland, Tauranga, Napier, and Lyttelton.
Consult with our senior structural storage engineers. Send us your warehouse floor plan, clear ceiling height, pallet dimensions, and target position counts to receive a comprehensive CAD design and factory-direct price estimation.
