Modern logistics operations face severe real-estate cost pressures and accelerating cubic-meter storage demands. Conventional selective pallet racking dedicates over 60% of floor space to static access aisles that remain idle 95% of the operational lifecycle. Electric Mobile Racks (also designated as Motorized Mobile Pallet Racking, Powered Mobile Compactors, or Intelligent Mobile Bases) resolve this volumetric bottleneck by mounting heavy-duty structural uprights onto motorized steel carriages running on precision-embedded floor rails. By opening a single dynamic aisle on demand via programmable logic controllers (PLC), mobile systems eliminate redundant access corridors, immediately unlocking up to 90% additional storage capacity within identical warehouse footprints.
From multi-ton palletized racking installations in sub-zero cold stores to high-precision voice-activated electronic compactors and specialized textile fabric roll carriers, our engineering systems are manufactured to stringent global mechanical standards.
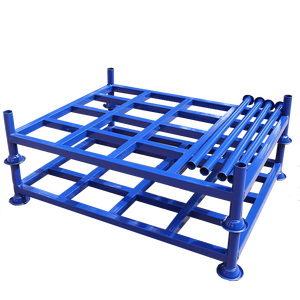
Designed for heavy textile rolls and cylindrical raw materials. Features modular stackability, high-load base beams, and anti-roll cradle geometry for bulk industrial staging.
View Technical Specs
Combines the direct-access accessibility of selective racking with mobile chassis flexibility. Built with cold-formed steel sections engineered for heavy forklift handling.
View Technical Specs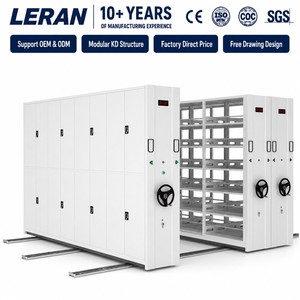
Integrated variable frequency electric drives, optical anti-crush safety sensors, electronic interlocks, and master PLC touchscreen consoles for automated density warehouses.
View Technical Specs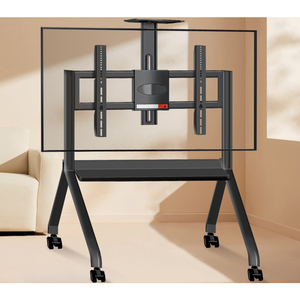
Precision motorized vertical lifting trolley with industrial-grade locking castors. Ideal for control rooms, warehouse dispatch dispatching monitoring, and corporate training hubs.
View Technical Specs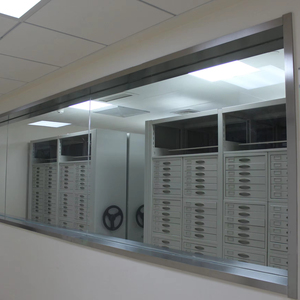
Equipped with offline voice recognition command processing, touch interface, automated gangway illumination, and dual-mode manual/electric override for rapid SKU picking.
View Technical Specs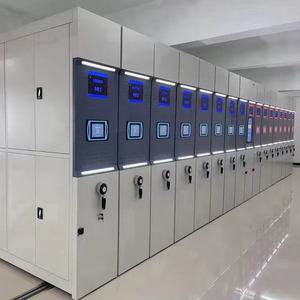
Engineered for legal, banking, hospital records, and confidential sample archiving. Incorporates biometric RFID access, auto-ventilation spacing cycles, and smoke sensor triggers.
View Technical Specs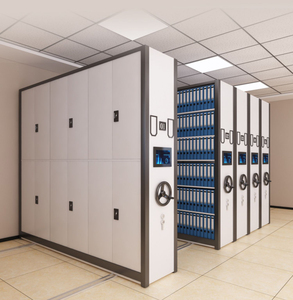
Features high-torque synchronous worm-gear drives, micro-pitch shelf adjustability, and anti-static architectural powder coating. Guarantees silent, jitter-free glide cycles.
View Technical Specs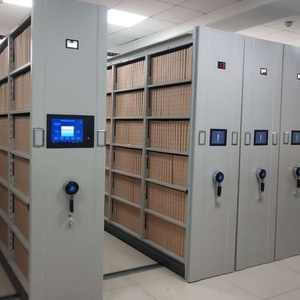
Built with cold-rolled SPCC steel frames, multi-column mechanical clutch decoupling, and software integration for real-time document location tracking and computerized audit trails.
View Technical SpecsIndustrial logistics engineering evaluates storage density through the lens of volumetric efficiency and cycle selectivity. In standard selective racking warehouses, up to 65% of the total cubic footprint is consumed by permanent corridors necessary for counterbalance forklifts, narrow aisle (VNA) trucks, or reach trucks to maneuver. Electric Mobile Racks revolutionize this spatial equation by arranging high-capacity racking runs onto heavy-duty structural steel carriages fitted with machined flanged steel wheels. These carriages travel smoothly along embedded precision guide rails embedded directly within the reinforced concrete floor slab.
When an operator demands access to a specific pallet location—via warehouse management software (WMS), vehicle-mounted radio-frequency terminals, or carriage-mounted ergonomic push buttons—the central PLC sends synchronized frequency-controlled drive commands to the integrated gearmotors. The mobile blocks silently glide open to expose a single wide working aisle (typically 3,000 mm to 3,500 mm, customized precisely to the turning radius of the forklift fleet). All other structural bays remain tightly locked in a dense, consolidated block.
| Storage Technology | Space Utilization | Pallet Selectivity | Cold Store Thermal ROI | Civil Floor Requirements | Operational Flexibility |
|---|---|---|---|---|---|
| Electric Mobile Racks | 85% – 90% (Ultra High) | 100% Direct Selective Access | Highest (-45% Energy Draw) | Embedded Precision Rails (DIN 18202) | Full pallet & mixed SKU picking |
| Standard Selective Racks | 35% – 40% (Poor footprint use) | 100% Direct Selective Access | Poor (Heats/Cools empty air) | Standard Commercial Slab | Universal but space wasteful |
| Drive-In Pallet Racks | 70% – 75% (High density) | LIFO Only (Honeycombing risk) | Moderate | Standard Slab + Heavy Upright Shrouds | Restricted to batch homogenous SKUs |
| Automated AS/RS Crane System | 90% – 95% (Maximum vertical) | 100% Computerized Access | High (Enclosed High-Bay) | Deep Pile Foundation + Silo Structure | High CapEx; inflexible to reconfigure |
Refrigerated and blast-freezer warehouses represent the highest per-cubic-meter operational cost in modern warehousing. Cooling refrigerated air within unoccupied static forklift aisles wastes colossal amounts of electric utility power. Electric Mobile Racks have become the baseline engineering requirement for global cold chain facilities operating between 0°C and -30°C.
By eliminating empty aisle volumes, the required refrigerated room envelope is reduced by up to 45% for the same pallet inventory. Less volume directly scales down refrigeration compressor tonnage, cutting ongoing electricity bills by up to 50%. Furthermore, advanced smart mobile controllers integrate an automated Night-Park Ventilation Sequence: at scheduled shifts or off-peak hours, the mobile bases automatically distribute themselves along the floor rails with equal 300 mm spacing gaps. This prevents cold air stratification, eliminates ice-frost buildup between packaging, and guarantees homogenous temperature gradients across sensitive pharmaceutical drugs, biologics, and frozen food SKUs.
Procurement engineers and supply chain executives must evaluate mobile racking investments across a 15-to-25-year structural lifecycle. Rapid advances in operational robotics, safety electronics, and carbon reporting are fundamentally transforming purchasing specifications worldwide.
Next-generation electric mobile bases incorporate smart vibration monitors, current draw sensors on gearmotors, and thermal probes on axle bearings. Data streamed via MQTT or OPC-UA to cloud platforms detects mechanical rail misalignment or motor wear weeks before any physical stoppage can trigger warehouse downtime.
Modern global safety compliance mandates multi-tier fail-safe architectures. Systems now pair full-height longitudinal photoelectric safety barriers at carriage base levels with active ultrasonic motion scanners and tactile emergency shutdown foot-bumpers (kickplates) to achieve SIL 3 / Performance Level d (PLd) certification.
The manual push of an aisle button is rapidly becoming obsolete. High-throughput facilities integrate automated guided vehicles (AGVs) and autonomous mobile robots (AMRs). The facility WMS automatically sends radio opening requests to the rack PLC while the robot is en route, eliminating vehicle queuing latency.
Procurement audits now evaluate the embodied carbon in structural steel. Sourcing specifications prioritize manufacturers utilizing certified low-emission electric arc furnace (EAF) structural steel (Q235B, Q355B, and EN 10025 grades) combined with solvent-free, heavy metal-free powder coating lines that pass stringent RoHS tests.
Moving 500 tons of racking mass requires controlled acceleration and deceleration ramps to prevent pallet shedding and structural racking fatigue. Modern variable frequency drives smooth the mechanical torque curve, utilizing kinetic deceleration regeneration to recycle dynamic braking power back into facility micro-grids.
Rather than relying on single centralized drive shafts, advanced mobile designs utilize modular direct-drive gearmotors mounted on individual wheel sets. This decoupled approach distributes torque evenly, prevents single-point mechanical shaft breakage, and allows uninterrupted emergency manual decoupling during complete electrical grid outages.
Founded in 1977, Divakaran Storage and Handling Systems Pvt. Ltd. operates dedicated in-house manufacturing facilities in Umbergaon, Gujarat, India. With more than four decades of dedicated metallurgical engineering and heavy-gauge steel forming, our products have earned a trusted reputation across India, Bahrain, Sri Lanka, Canada, and the wider Middle East.
We are a direct original manufacturer, not a broker. Complete end-to-end roll forming, CNC punching, precision welding, and robotic shot-blasting are executed under strict ISO quality controls at our Umbergaon plant.
Every upright column, box beam, and mobile carriage chassis is engineered using verified structural grade steel. Component thicknesses are calculated via finite element analysis (FEA) to exceed local seismic codes and payload ratings.
All mobile bases, beams, and upright trusses are designed as modular, bolt-together knock-down sub-assemblies. This achieves maximum container cube utilization for cost-effective sea freight to North America, Africa, and the GCC.
From preliminary civil floor flatness laser assessments and dynamic layout drafting to on-site installation supervisory engineers and 24/7 post-commissioning technical troubleshooting, we back every rack for decades.
Procuring high-density electric mobile racking involves complex interactions between structural civil engineering, electric drive controls, and logistics workflows. Here are the core technical answers every procurement team requires.
Plan your warehouse expansion with accurate load calculations, customized AutoCAD layout designs, and complete structural finite element analysis. Speak directly with our Umbergaon manufacturing engineering team today.
