Fabricated from premium cold-rolled Q235B and Q355B structural steel, conforming strictly to FEM 10.2.02, ANSI MH16.1, and AS4084-2023 international load standards.
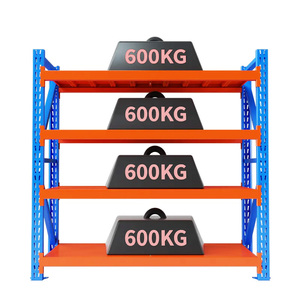
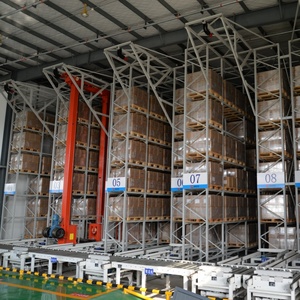
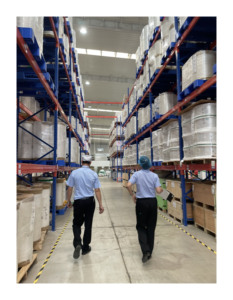
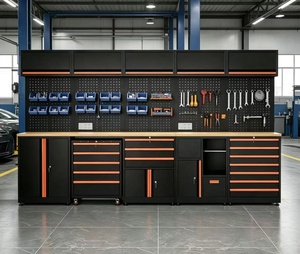
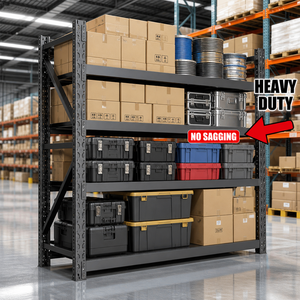
In contemporary supply chain logistics, warehouse storage systems are no longer treated as passive metal shelving; they are vital structural assets subjected to dynamic seismic forces, cyclical forklift mast impacts, and high cyclic load stresses. Procuring high-bay pallet racking and automated shuttle storage directly from China's premier manufacturing ecosystems requires an exhaustive understanding of metallurgical formulations, cold-forming cross-sectional geometries, and finite element stress modeling. High-density storage facilities operating at clear heights between 12 to 36 meters mandate extreme deflection thresholds—typically limited to L/200 under total working capacity—to prevent harmonic sway and frame destabilization during simultaneous crane or reach-truck operations.
The metallurgical baseline for industrial racking centers upon high-yield structural coil steels, specifically Q235B and Q355B (equivalent to ASTM A36 and ASTM A572 Grade 50 respectively). The continuous roll-forming lines operate through progressive cold-bending sequences containing up to 24 rolling stations. This multi-pass forming ensures that omega-shaped upright columns retain precise outer-edge radii without micro-cracking or residual tensile stress hotspots along the punched beam-locking teardrop or diamond perforations.
Furthermore, beam-to-column connectors represent the most crucial link in structural stability. Advanced Chinese manufacturing employs robotic weldments where cold-drawn steel connector teeth (typically 3-claw or 4-claw configurations) are MIG-welded to twin-C interlocking box beams. These connections produce high semi-rigid moment resistance, absorbing longitudinal dynamic thrusts without mechanical loosening. Automated pre-treatment featuring zinc-phosphate washing combined with electrostatic thermosetting epoxy polyester powder coating provides salt-spray resistance up to 500 hours, exceeding ASTM B117 international corrosion standards for industrial distribution facilities.
B2B Procurement Insight: The true cost of industrial warehouse storage is measured by structural yield safety margins, spatial density, and container stowage cubing efficiency. Knock-down modular components reduce maritime freight costs by up to 62% per pallet position compared to pre-assembled framework units.
Combining heavy metallurgical production scale with international safety certification, rapid prototyping, and end-to-end containerized logistics.
Every beam, upright frame, and diagonal bracing element utilizes certified Baosteel or Shougang hot-rolled prime coils, strictly lab-verified for chemical purity, tensile yield strength, and elongation resistance.
State-of-the-art rolling lines maintain tolerance limits within ±0.2mm across 12-meter continuous sections, guaranteeing instantaneous on-site bolt alignment and vibration-free stacker crane traveling.
Full manufacturing lifecycle certified under ISO 9001, ISO 14001, ISO 45001, CE EN 15512, and AS4084, complete with certified 3D FEA (Finite Element Analysis) load calculation reports for local regulatory approval.
From initial DWG warehouse layout optimization and pallet footprint analysis to knock-down export packing and dispatch of certified installation supervisors across North America, the Middle East, and Europe.
How global purchasing managers and supply chain directors are navigating automated high-cube racking, sustainability mandates, and dynamic inventory fluctuations.
The global shift away from conventional selective racking toward four-way automated pallet shuttles is revolutionizing storage density in both ambient and -25°C cold storage facilities.
Replacing traditional post-weld hot-dip galvanizing with pre-coated ZAM alloy steel for extreme corrosion resilience in chemical, coastal, and pharmaceutical environments.
Building the storage racking as the primary structural frame of the facility, where wall claddings and roofing are mounted directly onto the steel upright framework.
Quick cross-reference guide to select the right storage framework based on SKU variety, material handling equipment (MHE), and volumetric optimization.
| Storage Solution | Load Rating (Per Tier) | Selectivity Level | MHE Compatibility | Density Level | Primary Application |
|---|---|---|---|---|---|
| Selective Pallet Racking | 1,000 kg – 4,500 kg | 100% Direct (FIFO) | Counterbalance, Reach Truck | Standard | FMCG, Retail, 3PL Distribution |
| Drive-In / Drive-Through | 800 kg – 1,500 kg | Low Selectivity (LIFO) | Standard Counterbalance | Very High | Cold Stores, Beverage, Bulk SKUs |
| Radio Pallet Shuttle | 500 kg – 2,000 kg | Medium-High (FIFO/LIFO) | Reach Truck + Shuttle Cart | Maximum | Food Logistics, Fast Turnover Hubs |
| Automated AS/RS Stacker Crane | 500 kg – 3,000 kg | 100% Automated (WMS/WCS) | Stacker Cranes, Hoists | Extreme High-Cube | Smart Factories, Pharma, E-Commerce |
| Mobile Power Racking | 1,000 kg – 3,500 kg | 100% Access (Motorized Aisle) | Reach Truck, Forklift | +85% Footprint | High-Land Cost Cities, Cold Stores |
| Cantilever Storage Racks | 300 kg – 5,000 kg / Arm | Unobstructed Front Loading | Side Loader, Crane, Forklift | Linear Open | Pipes, Timber, Aluminum Profiles |
Technical considerations, container stowage calculations, customs clearance, and structural compliance for international racking buyers.
To provide an accurate structural proposal and CAD architectural drawing, our engineering team requires: (1) Architectural DWG plan indicating building column grids, interior clear ceiling heights, and door locations; (2) Pallet specifications including overall dimensions (W × D × H), overhang allowances, and gross weight per unit; (3) Type and technical specification sheet of Material Handling Equipment (turning radius, maximum mast elevation, and minimum aisle width requirement); and (4) Concrete floor slab thickness, slab rebar specifications, and local geotechnical seismic load parameters.
Our structural engineering team designs racking frameworks using customized software in full compliance with European EN 15512 / FEM 10.2.02 codes, American ANSI/RMI MH16.1 standards, and Australian AS4084-2023 regulations. We perform comprehensive finite element structural simulations covering moment rotation stiffness, lateral frame stability, and seismic base plate shear stresses. Mill test certificates (MTCs) conforming to EN 10204 Type 3.1 are supplied with each production batch verifying chemical and mechanical compliance.
Racking components are packaged as knocked-down units to maximize container cubic capacity while preventing galvanic corrosion or surface scratching. Upright frames are separated with protective plastic spacers and bundled with heavy-duty PET strapping. Box beams are packed on custom wood or steel pallets with corner angle protectors and stretch-wrapped in anti-moisture VCI film. Small accessories, fasteners, safety pins, and leveling shims are packed in double-walled corrugated cartons secured on reinforced wooden crates.
Standard production lead time for typical wholesale orders (2 to 5 full 40-foot HQ containers) ranges between 20 to 28 working days following final CAD drawing approval and deposit confirmation. For highly complex automated AS/RS or multi-tier mezzanine projects requiring custom tooling and high-precision laser-drilled structural tracks, production timelines are typically scheduled between 35 to 45 working days. Priority emergency production lines are available for urgent logistics infrastructure projects.
Yes, over 70% of our production volume operates under OEM/ODM contracts for international distributors, system integrators, and brand owners. We can match any specific RAL color palette (standard warehouse safety orange RAL 2004 and gentian blue RAL 5010 are popular defaults) using UV-resistant outdoor or food-grade indoor powder formulations. Custom hole punching patterns, company embossed logos on steel footplates, and private-label packaging are seamlessly integrated into our continuous production lines.
We provide comprehensive installation manuals, 3D exploded assembly diagrams, and high-definition video walkthroughs for every custom project. For high-bay AS/RS setups or projects exceeding 5,000 pallet positions, we deploy veteran installation supervisors and commissioning engineers to project sites globally to oversee ground anchoring, vertical plumbness calibration, stacker crane rail leveling, and electrical safety integration.
Whether planning a new regional distribution center, retrofitting high-density mobile racking, or installing a fully automated AS/RS high-bay system, our engineering design team delivers tailored layouts, structural load calculations, and competitive factory-direct wholesale pricing within 24 hours.
