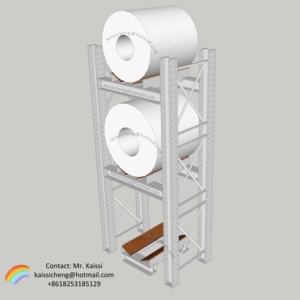
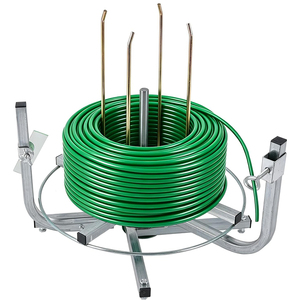
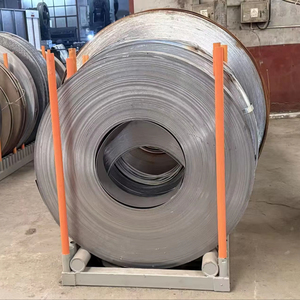
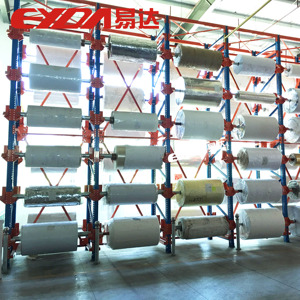
Configured for master steel coils, slit coils, copper rolls, cable reels, and logistics transport cradles. Compliant with strict CE execution standards and load-bearing dynamics.
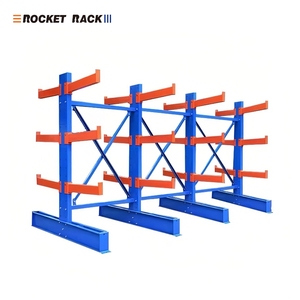
A comprehensive mechanical analysis of concentrated radial loads, yield deformation prevention, and seismic safety requirements for modern coil handling facilities.
Unlike palletized uniform distributed loads (UDL), a 25-ton cold-rolled steel coil exerts an extreme, tangential line contact along its cradle tangent. Without finite element analysis (FEA) calibrated saddle profiles, standard beams suffer from instantaneous flange buckling and web crippling.
Heavy overhead cranes and c-hook manipulators induce dynamic kinetic spikes during coil placement. Our engineering calculations mandate an impact factor amplification of $\psi \ge 1.35$ to $1.50$, preventing long-term structural fatigue in high-throughput stamping facilities.
Under European safety directives (Machinery Directive 2006/42/EC and EN 15512 for steel static storage systems), CE certified coil racks require factory production control (FPC), documented weld non-destructive testing (NDT), and traceable mill test certificates (MTC 3.1).
Cylindrical material handling introduces distinct challenges unseen in general warehouse racking. A master coil behaves as a rigid, heavy-gauge cylinder prone to lateral displacement and roll-out. The foundational challenge lies in the Hertzian contact stress generated along the saddle interface. When heavy wound metals (such as grain-oriented electrical steel, automotive galvanized coils, or heavy copper strips) are stacked vertically or seated on shallow angles, radial forces create an outward splitting vector on the rack uprights.
Our CE-certified coil storage racks utilize an engineered cradle saddle geometry angled precisely between $35^\circ$ and $42^\circ$. This specific angular spectrum creates a self-centering equilibrium: the inward vector generated by gravity neutralizes the lateral thrust force against the upright beams. Furthermore, to safeguard prime steel surfaces from indentation (which causes expensive scrap losses at automotive press lines), our contact surfaces feature vulcanized polyurethane, engineering synthetic polymer chocks, or oil-resistant ultra-high-molecular-weight polyethylene (UHMW-PE) liners.
Every structural profile utilized in our Umbergaon manufacturing plant undergoes rigorous physical and mechanical qualification. We utilize structural grade steel conforming to EN 10025-2 (S275JR and S355JR) with guaranteed yield strengths reaching up to $355 \text{ N/mm}^2$. Heavy structural hollow sections (HSS) and hot-rolled channel beams (UPN/HEA profiles) are deployed where maximum torsional resistance against asymmetrical impact is mandatory.
Welding integrity forms the backbone of CE compliance. Fabricated under ISO 3834-2 comprehensive quality requirements, all structural joints are executed by certified GMAW/FCAW welding operators. Ultrasonic (UT) and Magnetic Particle Inspection (MPI) testing are standard procedures on all primary cantilever arm brackets, stop pins, and baseplate butt welds, eliminating the risk of micro-fissuring and brittle fractures under cryogenic or heavy dynamic operating cycles.
Selecting the optimal coil storage configuration requires balancing floor footprint density, crane accessibility, inventory turnover velocity, and investment economics. Below is an engineering baseline comparison:
| System Architecture | Maximum Capacity / Level | Optimum Coil OD Range | Handling Interface | Floor Space Efficiency | Primary Regulatory Standard |
|---|---|---|---|---|---|
| Multi-Tier Cantilever Coil Racks | 15,000 – 25,000 kg | 800 mm – 2,200 mm | Overhead Crane / C-Hook / Ram Truck | Maximum (Vertical Cubing +300%) | EN 15512 / FEM 10.2.02 / CE |
| Heavy-Duty Ground Saddle Cradles | 35,000 kg per Bay | 600 mm – 2,500 mm | Overhead EOT Crane / Stacker Crane | Medium (Linear Floor Layout) | EN 1090-2 Class EXC2 / CE |
| Stackable Modular Interlocking Racks | 10,000 – 18,000 kg | 500 mm – 1,600 mm | Heavy Forklift / Telescopic Reach | High (Up to 4-Tier Free-Standing) | ISO 3834-2 / CE Marked |
| Logistics Dunnage & Transport Chocks | 5,000 – 12,000 kg / Pair | 400 mm – 1,800 mm | Chassis Mount / Flatbed Rigging | Transport Optimized (DOT / FMCSA) | DOT 49 CFR § 393.120 / CE |
Over 45 years of continuous industrial storage manufacturing from our Gujarat factory, delivering load-rated steel systems across five continents.
Founded in 1977, Divakaran Storage and Handling Systems Pvt. Ltd. operates dedicated structural fabrication facilities at C1/16 & 17, G.I.D.C. Industrial Estate, Umbergaon. We are authentic original equipment manufacturers (OEM)—never brokers or middle-tier agents.
Every beam, gusset, and upright is fabricated from tested high-tensile structural steel plates and channels. Sourced with complete chemical composition and elongation test certificates, ensuring ductile behavior without catastrophic brittle shear under peak impact.
Heavy capital investment in CNC multi-axis drilling, automated plasma plate profile cutting, and multi-station roll-forming lines ensures hole-pitch accuracy within ±0.5mm across 12-meter columns, guaranteeing seamless on-site bolt-together erection.
Our coil and heavy-duty storage installations operate reliably across Bahrain, Sri Lanka, Canada, UAE, Saudi Arabia, and Europe. Systems are engineered as Completely Knocked-Down (CKD) components optimized for high-cube container utilization without ocean shipping damage.
Our application engineers model your coil outer diameters, bore IDs, face widths, and bridge crane swing limits before metal fabrication commences. We provide full 3D assembly shop drawings, third-party load calculations, and long-term inspection protocols under EN 15635.
How progressive industrial supply chains are integrating automated vertical stacking, real-time stress telemetry, and zero-defect surface preservation.
Procurement directors are increasingly mandating optical fiber Bragg grating (FBG) or digital strain gauges integrated directly into cantilever bases. These sensors transmit real-time deflection telemetry, providing automated predictive alerts if dynamic loading exceeds safe design thresholds.
Manual floor storage is rapidly yielding to Automated Storage and Retrieval Systems (AS/RS). Modern CE-certified coil racks feature robotic locating dowels, vision-guidance targets, and millimeter-precision saddle pockets designed for unmanned automated guided vehicles (AGVs) and heavy stacker cranes.
As high-value silicon electrical steel (for EV drivetrains) and ultra-thin aluminum foil stocks proliferate, mechanical edge protection is mission critical. Modern procurement specifications dictate modular elastomeric saddle inserts with shore hardness ratings calibrated to eliminate all edge burring and coil ovalization.
European and North American buyers are aligning procurement frameworks with carbon footprint thresholds. Racking manufacturers must verify steel billet origin, electric arc furnace (EAF) scrap percentages, and eco-friendly thermosetting powder coating processes that emit zero volatile organic compounds (VOCs). Divakaran's production methodology emphasizes material optimization through cold-formed high-strength alloys—providing higher load capacities while reducing total steel consumption by up to 18% compared to obsolete, non-optimized hot-rolled structures.
Industrial manufacturing plants frequently alter their strip slit widths and master coil diameters based on fluctuating end-user orders. Monolithic, fully welded coil stands are being phased out in favor of bolted modular saddle systems. By utilizing standardized laser-slotted horizontal beams, warehouse operations can adjust cradle pocket widths in 50mm increments in minutes, accommodating diverse strip slitting runs without requiring secondary hot work permits or structural modifications.
Detailed answers prepared by our senior engineering division to assist international procurement managers and warehouse project leads.
Send your coil dimensions, maximum tonnages, and warehouse drawings. Our structural engineering team will prepare a preliminary layout and structural quotation within 24 business hours.
